Compare powder sachet machines
Review auger and related powder routes against bulk-density change, cohesion, dust and target commercial measure.

Powder flow and dosing
Difficult powders are packed by controlling the complete path from bulk transfer to hopper, auger or alternative dosing device, product drop and seal area—not by changing the filler setting alone.
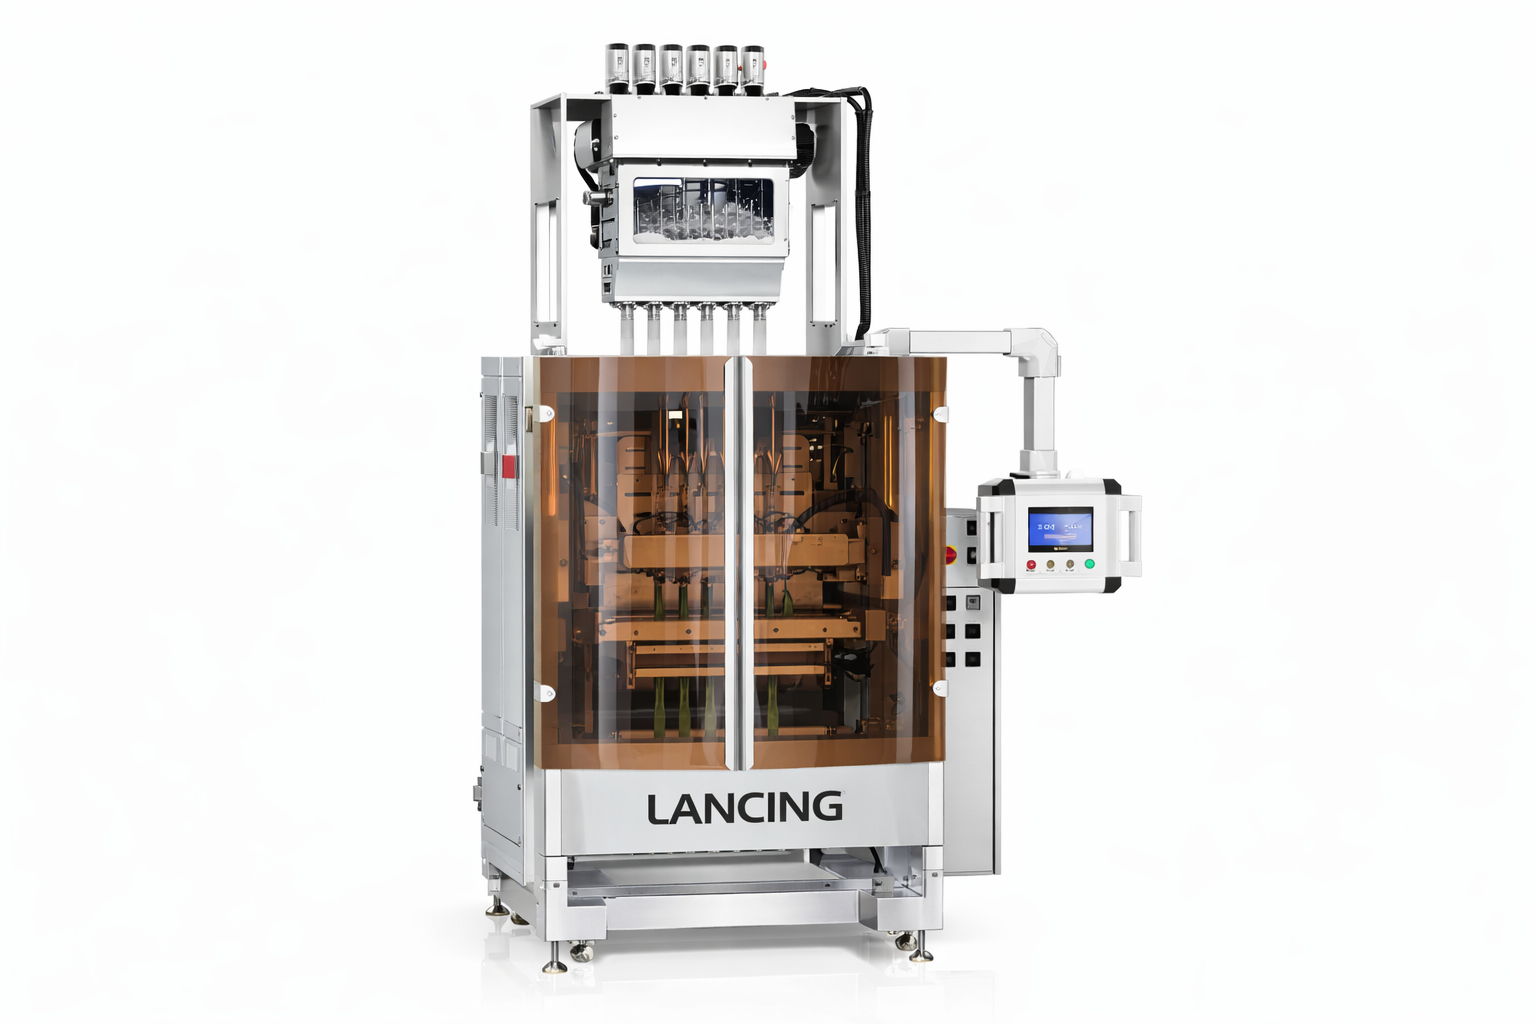
To pack a dusty or poor-flowing powder, define how it compacts, aerates, bridges, rat-holes and changes bulk density, then select and test the hopper, agitation, feeder, auger or other dosing method with the intended transfer and refill process.
The machine must also keep dust away from the film path, sensors and sealing jaws. A result obtained by hand-feeding a small settled sample directly into the dosing head does not prove production performance if the real process uses a vacuum feeder, screw conveyor or bulk bag discharge.
Poor flow is a broad description of inconsistent movement; bridging is a stable arch over an outlet; rat-holing is a narrow flow channel that leaves stagnant powder around it.
Each can create different dose symptoms. Bridging may produce sudden low or empty packs, while rat-holing can allow a temporary flow that collapses after the central channel empties. Photographs of a powder pile are not enough—observe the product in the intended hopper geometry and level range.
An auger delivers a controlled geometric volume, so a change in the mass occupying that volume changes the pack weight unless the control method compensates.
Powder can become aerated during transfer or compact under vibration and residence time. Record loose, transferred and settled conditions where relevant. The acceptance plan should specify when samples are taken after refill and how any feedback or checkweighing system is used.
Refill can change pressure above the auger, aeration, compaction, agitation load and the distribution of product around the outlet.
A feeder that delivers powder in large pulses may create larger dose transients than a controlled demand system. Test at high, normal and low hopper levels and retain sequential packs around refill. Stable results from the middle of a hopper do not establish the response at the boundaries.
The feed system should maintain a defined hopper level or demand range without excessive aeration, segregation, compaction or uncontrolled dust release.
Its capacity, transfer method, product-low logic, cleanability and interface signals must match the sachet machine. The supplier boundary should identify who provides the feeder, support structure, extraction connection, level sensors and safe access for cleaning or blockage clearance.
Trace when and where powder leaves the controlled drop path, then relate contamination to fill timing, product fall, air movement, film motion, overfill and hopper or feeder events.
Do not begin by increasing seal temperature. Dust between the sealant layers can prevent full contact even when the jaws are hot. Use lane- and time-identified retained packs, inspect jaw and film surfaces, and compare stable operation with refill, stop and restart.
| Trial condition | What it reveals | Evidence |
|---|---|---|
| Production-intent transfer | Aeration, compaction and feeder behaviour | Feed method, hopper level and sequential dose data |
| High-to-low hopper level | Pressure and flow changes | Samples by level and lane |
| Refill event | Transient bulk-density or flow disturbance | Packs before, during and after refill |
| Pause and restart | Settling, bridging and first-dose response | Alarm/state record and first accepted pack |
| Cleaning/changeover | Access, retained powder and reassembly repeatability | Procedure timing and post-change verification |
Related answers
Review auger and related powder routes against bulk-density change, cohesion, dust and target commercial measure.
Connect hopper conditioning, agitation, screw geometry and refill control to the intended mass or volume result.
Trace product carry-over, headspace, timing and cut-off before changing the sealing process.
Provide production-representative powder, transfer details, dose range, film and acceptance criteria for testing.
Apply the answer to your production case
Provide representative product, dose range, sachet drawing, film or artwork data, target accepted output and the site or line constraints that affect the answer. Lancing Ltd can then identify the machine route and evidence still required before quotation.